Discover latest news, architectural innovations, and expert perspectives on modular steel-frame construction across Europe.
Factory-engineered volumetric modules designed for high-density particle control, rapid on-site assembly, and full compliance with European ISO 14644 and cGMP regulations across Hungarian industrial parks.
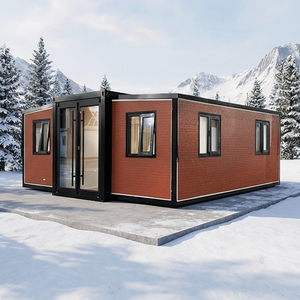
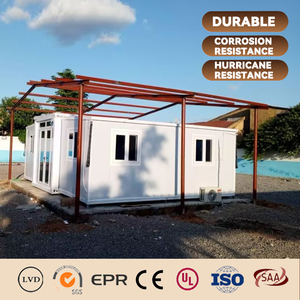
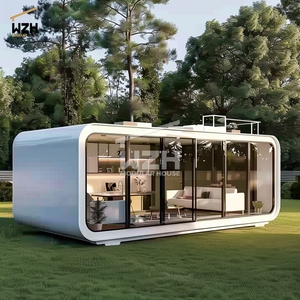
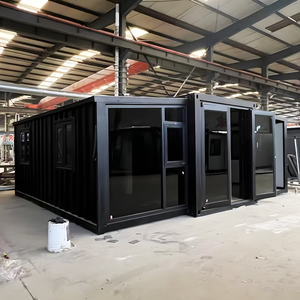
A Technical Whitepaper on Volumetric Off-Site Modular Construction for High-Precision Contamination Control Environments
Hungary has positioned itself as the preeminent manufacturing epicenter of Central and Eastern Europe (CEE). Driven by massive foreign direct investment (FDI) in electric vehicle (EV) battery mega-factories, automotive electronics, biotechnology, and specialized pharmaceuticals, the demand for high-performance controlled environments has surged exponentially. Traditional stick-built cleanrooms—characterized by lengthy on-site construction cycles, extensive dust generation, unpredictable labor scheduling, and chaotic trade overlaps—no longer align with the compressed commissioning schedules required by global tech giants operating in Hungary.
Prefabricated volumetric cleanroom modules represent a paradigm shift. Utilizing Design for Manufacture and Assembly (DfMA) principles, cleanroom spaces are precision-engineered, structurally framed, and fully assembled within a controlled factory environment. Wall paneling, walk-in ceiling grids, HVAC plenum integration, electrical raceways, and sanitary epoxy/PVC flooring are installed under strict ISO 9001 quality supervision prior to transport. This off-site approach decoupled civil site preparation from cleanroom envelope fabrication, collapsing total project schedules by 30% to 50%.
Unlike standard modular containers, industrial volumetric cleanroom pods utilize heavy-gauge zinc-coated structural steel chassis designed to resist micro-vibrations—a critical parameter for semiconductor photolithography and battery cathode slurry coating. Wall systems incorporate high-density Polyisocyanurate (PIR) or hydrophobic Rockwool cores wrapped in 0.8mm pre-painted galvanized steel (PPGI) or High-Pressure Laminates (HPL), achieving thermal insulation values down to U = 0.22 W/m²K while satisfying stringent EU fire resistance ratings (REI 60 / REI 120).
To meet international standards—specifically ISO 14644-1 through 14644-4 and the updated EU GMP Annex 1 guidance—our volumetric modules integrate three foundational architectural pillars:
Contamination control relies heavily on geometry. Our modules eliminate internal ledges, exposed fasteners, and right-angle junctions. Wall-to-wall, wall-to-ceiling, and wall-to-floor intersections are equipped with extruded aluminum or radius PVC coving. Double-glazed flush window units are integrated directly into sandwich panels with internal desiccant buffers to prevent condensation during thermal cycling. Panel joints are sealed using medical-grade, non-outgassing antimicrobial silicone or silicone-free cold-welding compounds, ensuring airtight performance under positive or negative room pressurization (ranging from 10 to 45 Pascals).
Cleanroom integrity depends entirely on thermodynamic stability and directional airflow control. Prefabricated modules are configured with built-in air handling units (AHUs) or direct plenum connections featuring multi-stage filtration (G4 pre-filters, F9 intermediate filters, and H14/U15 HEPA/ULPA terminal filters). For pharmaceutical operations requiring strict EU GMP Annex 1 compliance, airflow velocities are regulated at 0.45 m/s ± 20% for unidirectional laminar airflow zones (Grade A), while turbulent flow areas (Grade B-D) utilize variable air volume (VAV) dampers to maintain precise air exchange rates (AER) from 20 to 60+ air changes per hour.
Walkable ceiling grids constructed from heavy-duty aluminum T-bar profiles or sandwich structural cassettes allow maintenance personnel to service Fan Filter Units (FFUs), lighting fixtures, and gas/water pipelines from the technical mezzanine without stepping inside the sterile envelope. Electrical cabling, process gas manifolds (Nitrogen, Compressed Air, Argon), and purified water (PW) drop lines are pre-routed through factory-installed utility chases embedded directly within the panel cores, drastically reducing field-wiring time in Hungarian manufacturing plants.
| Evaluation Parameter | Factory Prefabricated Volumetric Modules | Traditional On-Site Stick-Built Cleanrooms |
|---|---|---|
| On-Site Construction Schedule | Rapid (4–8 Weeks On-Site) | Extended (6–12 Months On-Site) |
| Quality & Particle Control | 100% Factory Controlled ISO 9001 Assembly | Subject to On-Site Dust, Humidity & Trade Overlaps |
| Environmental Risk Mitigation | Pre-validated off-site; zero impact on active facility operations | High risk of cross-contamination in working plant |
| Commissioning & Qualification | Factory Acceptance Testing (FAT) completed prior to shipping | Qualification (IQ/OQ/PQ) entirely executed on-site |
| Flexibility & Relocation | Fully demountable, reconfigurable, and relocatable | Permanent construction; demolition required for changes |
| Thermal & Energy Efficiency | Monolithic insulated panel seal with U ≤ 0.22 W/m²K | Variable insulation gaps and potential thermal bridging |
Tailored engineering configurations designed to satisfy the rigorous technical requirements of Hungary's core industrial corridors.
Scenario: High-volume cathode slurry, cell assembly, and electrolyte filling in the Debrecen Southern Industrial Park.
Technical Solution: Specialized ultra-low humidity dry rooms integrated into volumetric modules. Engineered to maintain tight dew points down to -60°C and ISO Class 7/8 particulate standards. Walls feature chemical-resistant HPL faces resistant to aggressive solvents and NMP (N-Methyl-2-pyrrolidone) vapors.
Scenario: Sterile fill-finish operations, biological manufacturing, and API processing facilities.
Technical Solution: EU GMP Annex 1 Grade A/B compliant modular suites equipped with dynamic pressure cascades, interlocking airlocks (PAL/MAL), automated misting showers, and integrated Vaporized Hydrogen Peroxide (VHP) bio-decontamination systems.
Scenario: SMT assembly, MEMS sensor packaging, and LiDAR optical manufacturing.
Technical Solution: ISO Class 5 and 6 modular cleanrooms designed with dissipation conductive ESD epoxy flooring (10^6 to 10^9 ohms resistance), low-outgassing ceiling materials, and anti-vibration structural isolated sub-floors to maintain optical alignment.
Scenario: BSL-2 and BSL-3 diagnostic laboratories, gene therapy research, and medical device manufacturing.
Technical Solution: Negative pressure containment modules featuring exhaust HEPA filtration with safe-change bag-in/bag-out (BIBO) housings, airtight hermetic sliding doors, and complete chemical-resistant panelling.
Navigating EU Directives, National Building Standards (OTÉK), and Industrial Decarbonization
The revised EU GMP Annex 1 guidelines mandate an operational Contamination Control Strategy (CCS). Prefabricated cleanroom modules eliminate surface micro-fissures and poor joint geometries, providing validated continuous environmental monitoring (EMS) integration out-of-the-box.
Global supply chain realignments have driven massive industrial re-shoring to Northern Hungary (Miskolc, Nyíregyháza). Manufacturers cannot afford 12-month cleanroom builds. Off-site prefabrication allows factories to achieve commercial production 6 months ahead of competitors.
Energy costs across CEE have highlighted the need for efficient industrial HVAC. Our cleanroom modules utilize recirculating Fan Filter Units with EC (Electronically Commutated) motors and dynamic heat recovery wheels, slashing HVAC power consumption by up to 35%.
Building industrial infrastructure in Hungary requires full compliance with national fire protection codes (OTSZ) and local building authorities (OTÉK). Prefabricated modular cleanrooms manufactured in certified factories are supplied with full Eurocode structural engineering calculations (EN 1991, EN 1993), simplified fire safety certificates, and factory CE marking.
Because the internal cleanroom envelope can be classified as secondary self-supporting modular equipment within a primary industrial warehouse, permitting times are reduced dramatically compared to traditional permanent brick-and-mortar extensions.
Delivering uncompromised precision engineering, financial risk mitigation, and end-to-end turnkey execution.
Engineered using advanced Building Information Modeling (BIM) level LOD 400. Fabrication occurs entirely within ISO 9001, ISO 14001, and ISO 50001 certified manufacturing plants, eliminating weather delays and field error margins.
Fixed-price procurement contracts protect project budgets from inflationary material price spikes and field labor overruns. Guaranteed delivery schedules ensure reliable commissioning milestones.
Every modular cleanroom undergoes rigorous Factory Acceptance Testing (FAT) before shipment. We provide full IQ/OQ/PQ protocol documentation packages compliant with FDA 21 CFR Part 11 and EU GMP standards.
Direct answers to critical questions regarding logistics, compliance, customization, and thermal performance for cleanroom deployments across CEE.
Modules are engineered to standard volumetric transport dimensions compatible with European low-boy trailers and transit corridors (such as the M1, M3, and M5 motorways in Hungary). Upon arrival at your site—whether in Debrecen, Győr, or Budapest—the modules are offloaded via mobile crane, positioned inside your existing hall or on a concrete slab, bolted together, and sealed. Mechanical, electrical, and plumbing (MEP) connections feature quick-connect interfaces for rapid hookup.
Yes. We engineer specialized Dry Room volumetric pods featuring continuous vapor-barrier sandwich panel systems, continuous welded stainless steel or specialized joint sealants, and integration with desiccant dehumidification units. Our dry rooms maintain room dew points down to -60°C (equivalent to less than 0.5% relative humidity) necessary for moisture-sensitive lithium cell assembly.
Our prefabricated systems cover the complete cleanliness spectrum defined by ISO 14644-1, from ISO Class 3 / Class 5 (suitable for semiconductor photolithography and microelectronics) up to ISO Class 8 (general industrial assembly). For pharmaceutical customers, we deliver rooms fully qualified to EU GMP Annex 1 Grade A, B, C, and D operational standards.
All wall and ceiling panels utilize core materials certified under European fire standards (EN 13501-1) with ratings such as B-s1, d0 for PIR sandwich panels or A2-s1, d0 (non-combustible) for Rockwool panels. Structural steel chassis can be treated with intumescent coatings to achieve EI 60 to EI 120 fire resistance ratings, satisfying local Hungarian disaster management (Katasztrófavédelem) authority requirements.
We supply a complete validation master package comprising Design Qualification (DQ), Installation Qualification (IQ), and Operational Qualification (OQ) protocols. This includes material compliance certificates (REACH, RoHS), panel outgassing reports, HEPA filter integrity test certifications (DOP/EMERY tests), room pressurization maps, and air change rate verifications.
Absolutely. One of the core technical advantages of volumetric prefabrication is modular flexibility. If your production line needs to expand or shift, panels and structural modules can be unbolted, extended, or reconfigured with minimal downtime and zero destructive demolition dust inside your operating plant.
While traditional cleanroom construction takes 9 to 14 months, our modular off-site workflow delivers a fully functional, validated cleanroom in 12 to 18 weeks total. Factory manufacturing of the cleanroom pods occurs concurrently while your civil contractor prepares the site foundation and utilities in Hungary.
Planning a new production line or facility upgrade in Budapest, Debrecen, Győr, or across Central & Eastern Europe? Contact our cleanroom engineering team today for technical layout assistance, ISO/GMP compliance mapping, and budget estimates.